
In thin-film deposition processes, the dimensional selection of sputtering targets is often the first issue encountered by procurement and process engineers. Whether building a laboratory magnetron sputtering system or maintaining the coating throughput of a large-scale production line, the diameter, thickness, and planar dimensions of a target must strictly match the equipment cathode. Since targets are consumables and often require custom manufacturing, understanding the industry’s common dimensional conventions can significantly shorten procurement cycles and reduce processing costs.
1. Why Is There No Single “Standard Size” for Sputtering Targets?
The geometry of a sputtering target is fundamentally determined by the magnetron cathode structure of the sputtering system. Different equipment manufacturers use different target gun interfaces, cooling water channels, and shield gaps, so there is no globally universal dimensional system like those for screws or flanges. What is called a “common size” usually refers to specifications that most equipment manufacturers offer by default and that target suppliers keep in stock, mainly serving R&D and small-batch production. For industrial large-area coating, dimensions are often customized to the production line, with individual side lengths exceeding one meter.
2. Round Targets: The Mainstream Specification for R&D and Small-Area Coating
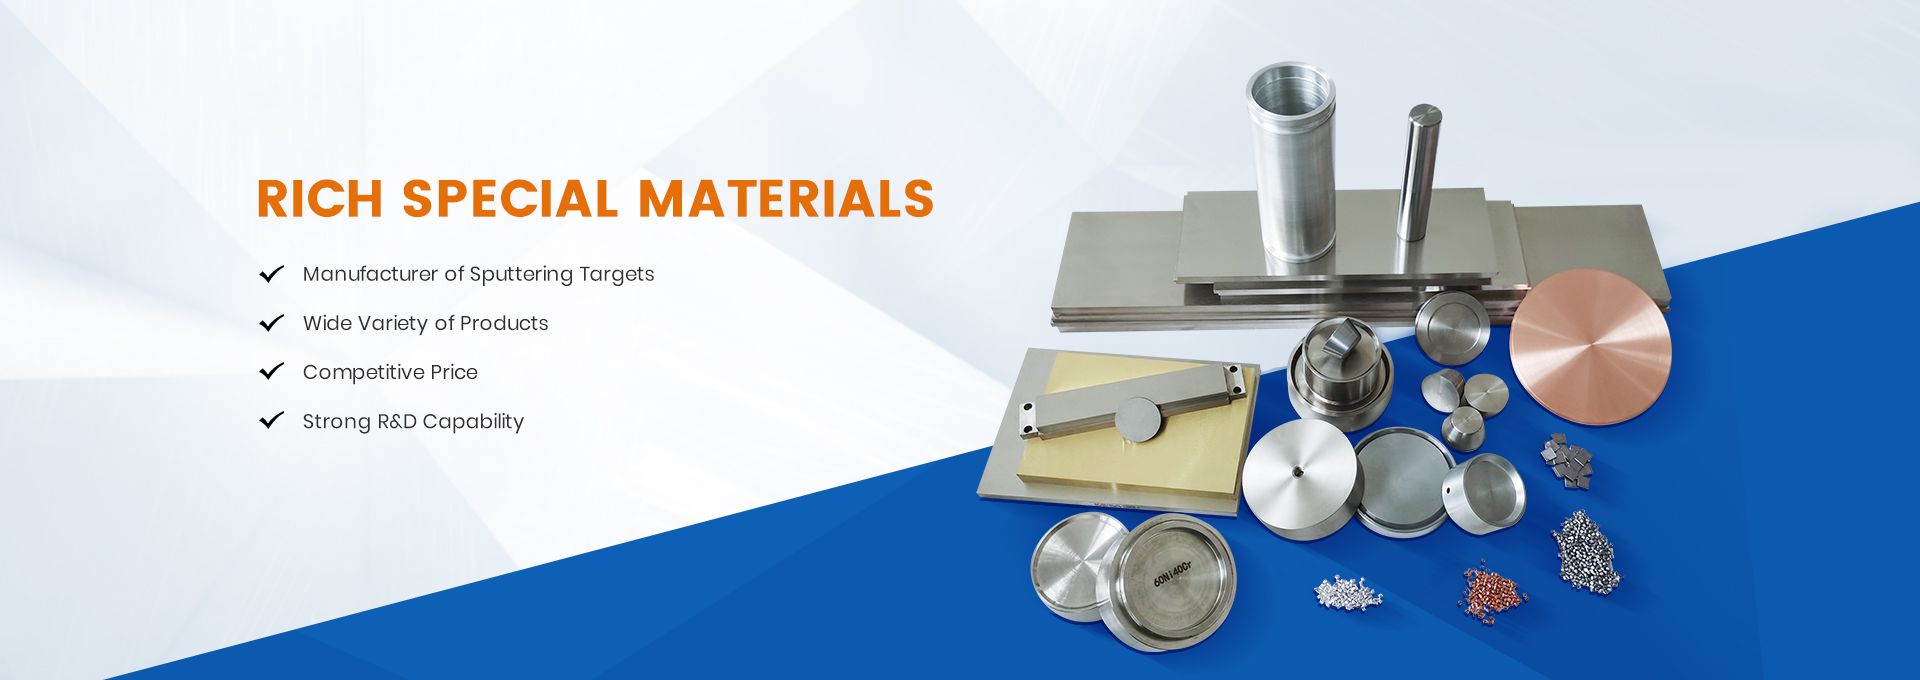
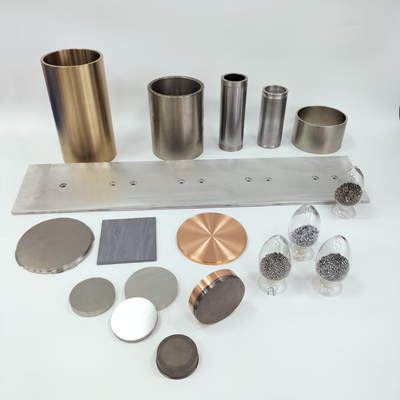
Round targets are the most common form in laboratory and R&D magnetron sputtering systems, with common diameters concentrated between 1 inch and 4 inches.
In imperial specifications, 2 inches (approximately 50.8 mm) is the most widespread R&D size. The standard target guns of many international equipment manufacturers are based on 2 inches, with typical thicknesses of 2 mm to 4 mm. For example, copper, aluminum, titanium, and ITO targets commonly seen in research procurement are often specified as φ50.8×3 mm or φ50.8×4 mm. 3 inches (76.2 mm) and 4 inches (101.6 mm) are used for experiments or small-batch trial production requiring slightly larger area uniformity, with thickness generally increasing somewhat with diameter, commonly 3 mm to 6 mm.
In the metric specification system, suppliers often label in whole millimeters, such as φ50 mm, φ60 mm, φ76.2 mm, φ100 mm, and φ101.6 mm. Standard round target diameters offered by high-purity material suppliers can cover φ50.8 mm to over φ300 mm, but large-diameter round targets are mostly used in specific optical coating or special industrial chambers and are not general R&D items.
For special applications, such as electron microscopy sample preparation or precious metal thin targets, thicknesses can be as thin as 0.1 mm to 1 mm, and diameters may use specific specifications such as 25 mm or 57 mm.
3. Rectangular Targets: The Core Form for Industrial Large-Area Coating
When the coating object is a glass substrate, display panel, or flexible substrate, the uniformity of round targets struggles to meet large-area requirements, and rectangular planar targets become the mainstream choice.
The common planar dimensions of industrial rectangular targets are usually characterized by length and width. Common standard planar specifications include 127×304.8 mm, 127×381 mm, and 127×508 mm, with thicknesses mostly of 3 mm, 5 mm, or 6.35 mm. In the domestic target supply system, laboratory or small industrial machines can also use 50×50 mm or 100×100 mm square targets for exploratory process development, while mass production lines use 300×300 mm or even longer custom dimensions.
It should be noted that the “common sizes” of rectangular targets are far less uniform than those of round targets. Target dimensions for architectural glass coating lines and display panel production lines are often tied to chamber width and transfer timing, making them equipment-specific custom parts that suppliers process to drawings rather than keep in stock.
4. Cylindrical Targets and Special Shapes
Cylindrical rotary targets mainly serve high-throughput industrial coating scenarios, with the advantage of much higher material utilization than planar targets (rotary use avoids the “race-track” erosion pits of planar targets). Common specifications are expressed as outer diameter × length, such as cylindrical targets with an outer diameter of 70 mm or 100 mm and a length of 100 mm to 2000 mm. Such targets are rarely used for R&D, and selection requires matching the end structures and cooling methods of the rotary cathode.
In addition, special-shaped parts such as ring targets and elliptical targets appear only in specific optical or semiconductor equipment and are usually customized to the original equipment manufacturer’s drawings, without a general dimensional series.
5. Key Matching Points During Selection
Before determining dimensions, several details that are easily overlooked but directly affect performance deserve priority confirmation.
Matching of thickness and cooling. Target thickness is not arbitrary and must match the cathode’s cooling water channels and magnetic circuit gap. An excessively thick target may reduce sputtering efficiency or cause insufficient cooling, while an excessively thin one may have too short a service life. The common thickness range for R&D round targets is 1 mm to 6 mm, while industrial targets have a wider range depending on the target gun design.
The metric-imperial conversion trap. A large number of imported devices use imperial interfaces, such as a 2-inch target actually corresponding to 50.8 mm rather than 50 mm. If a φ50 mm target is forcibly loaded into a 2-inch target gun during procurement, insufficient cooling or arcing may occur due to the smaller diameter. Research procurement lists explicitly specify φ50.8 mm rather than φ50 mm precisely to avoid this deviation.
The trade-off between customization and stock. 2-inch and 3-inch round targets and a small number of common planar sizes usually have stock or short lead times and lower prices. Once these common specifications are deviated from, even by only a few millimeters in diameter or thickness, custom manufacturing to drawings is often required, with lead times starting from several weeks and significantly higher costs.
Conclusion
The common dimensions of sputtering targets can be summarized as: for R&D, look at round targets, with 2 inches as the general benchmark; for industry, look at rectangular targets, with length customized to the line. The φ50.8 mm, φ76.2 mm, and φ101.6 mm of round targets and the 127 mm-wide series of rectangular targets constitute a de facto “common specification library.” During selection, priority should be given to confirming the original specifications of the equipment cathode interface (rather than simple conversion), and during the R&D stage, choosing common sizes with stock as much as possible is a pragmatic approach to balancing cost and efficiency. For industrial production lines, targets should be regarded as part of the equipment tooling and purchased as custom parts according to the original manufacturer’s drawings, rather than trying to find “universal parts.”
Post time: Oct-17-2026